Product
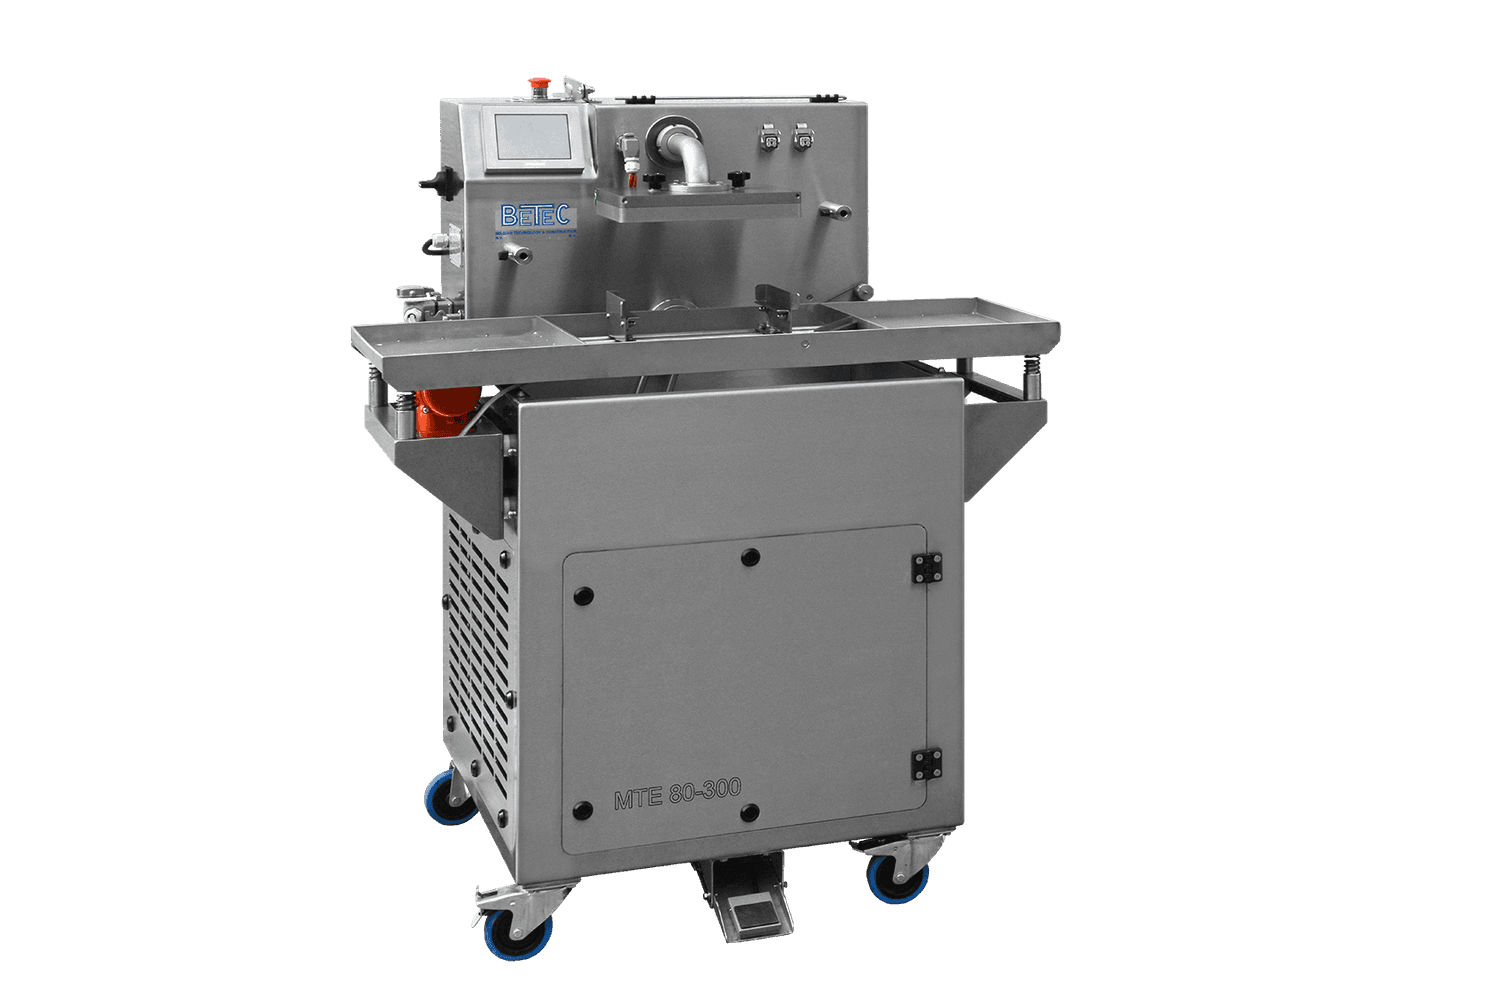
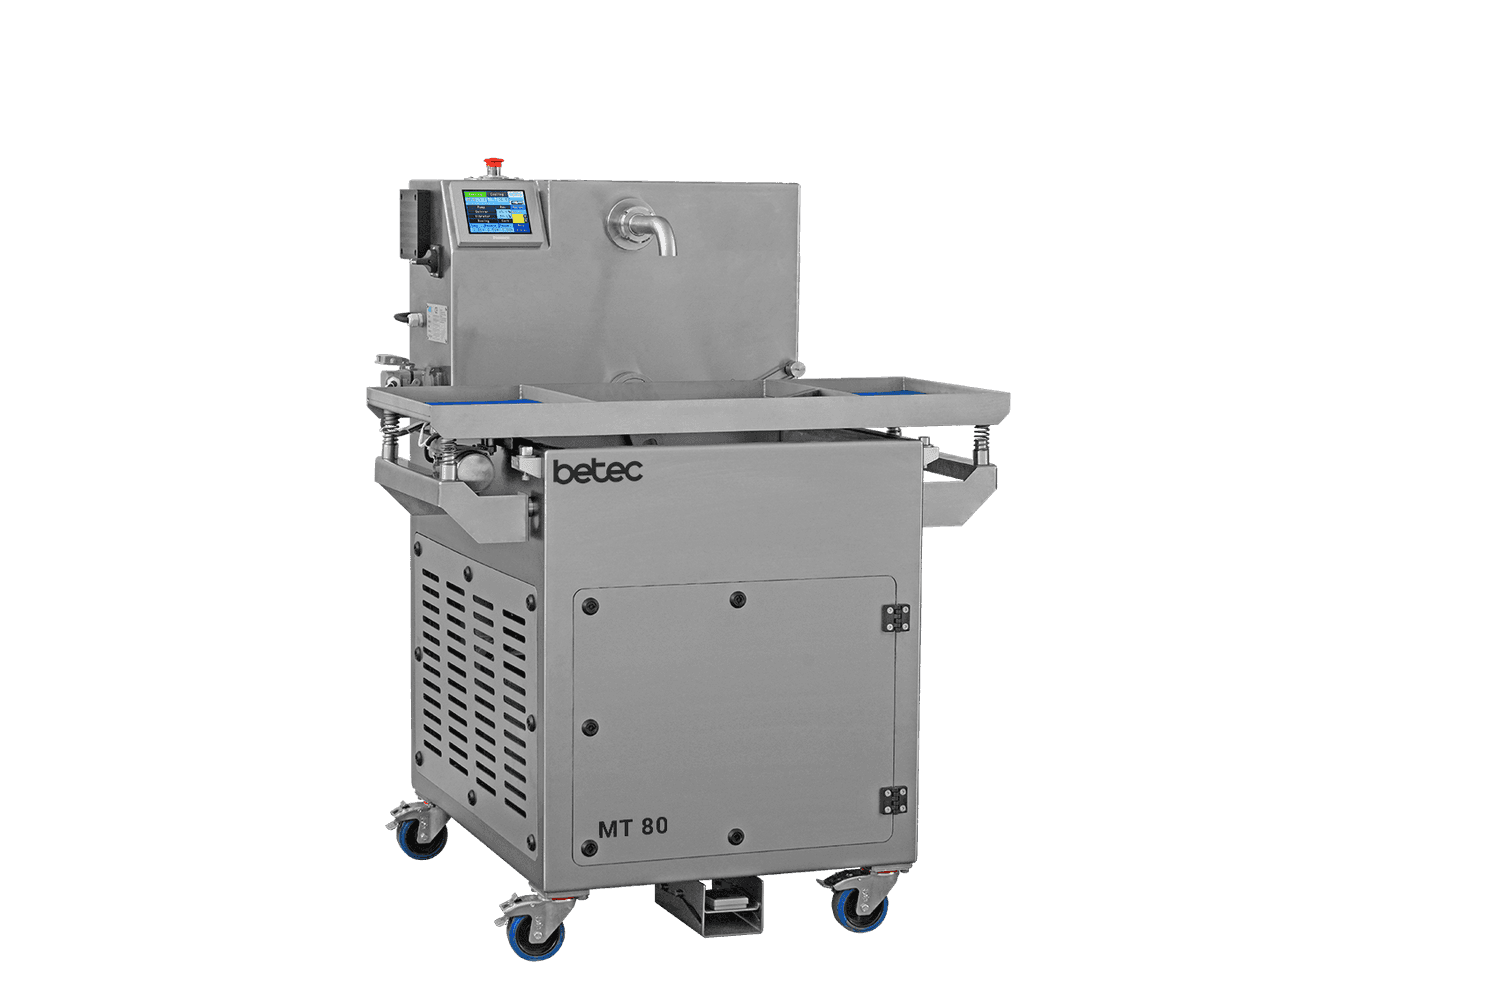
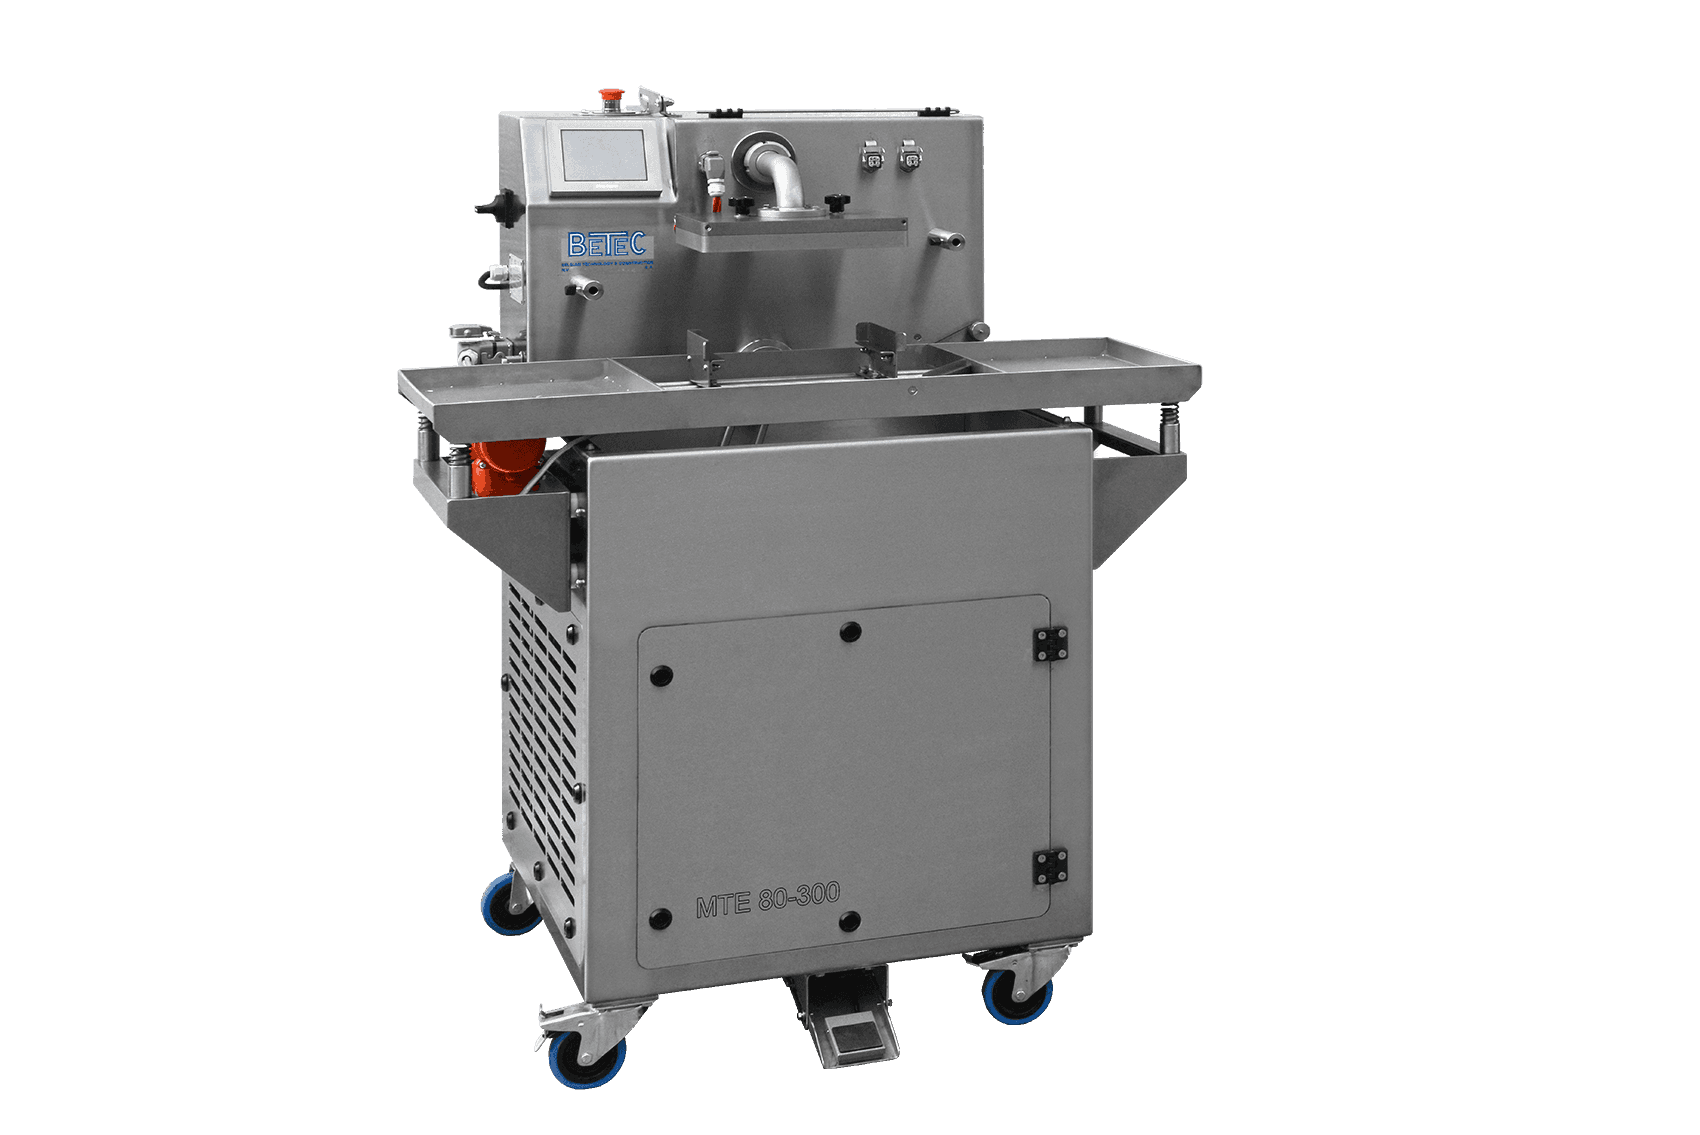
The BETEC MT/MTE 80 is the largest version in our MT/MTE series. Its 80 kg chocolate capacity and larger working zones on the vibrating table and enrobing belt suit larger artisan production volumes and applications requiring higher chocolate consumption and a larger chocolate supply.
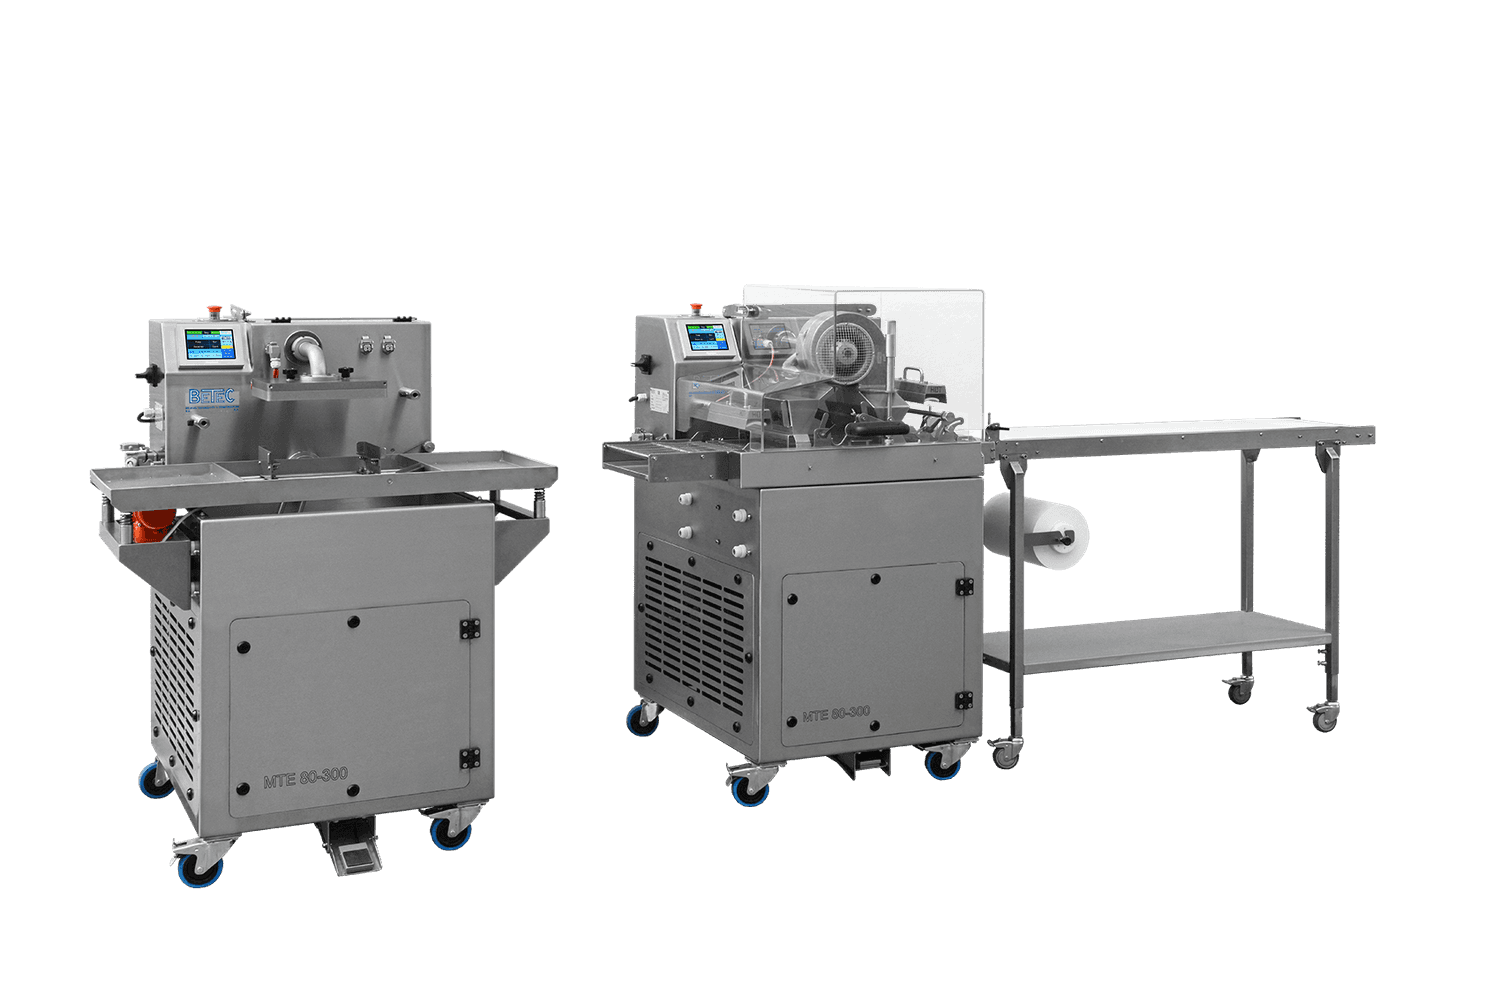
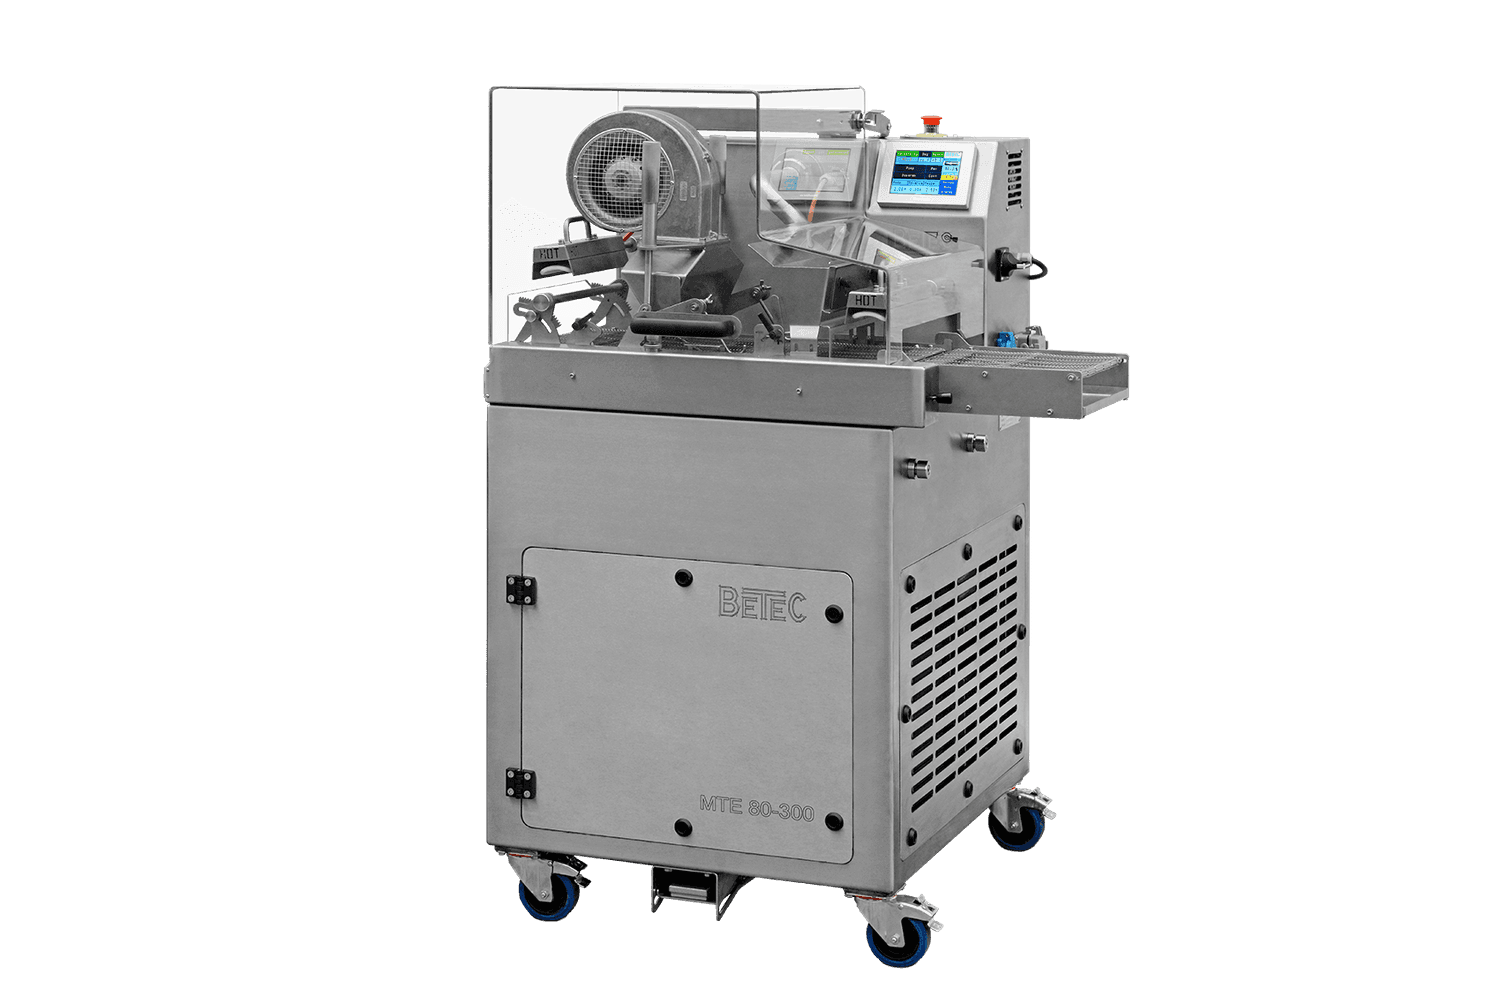
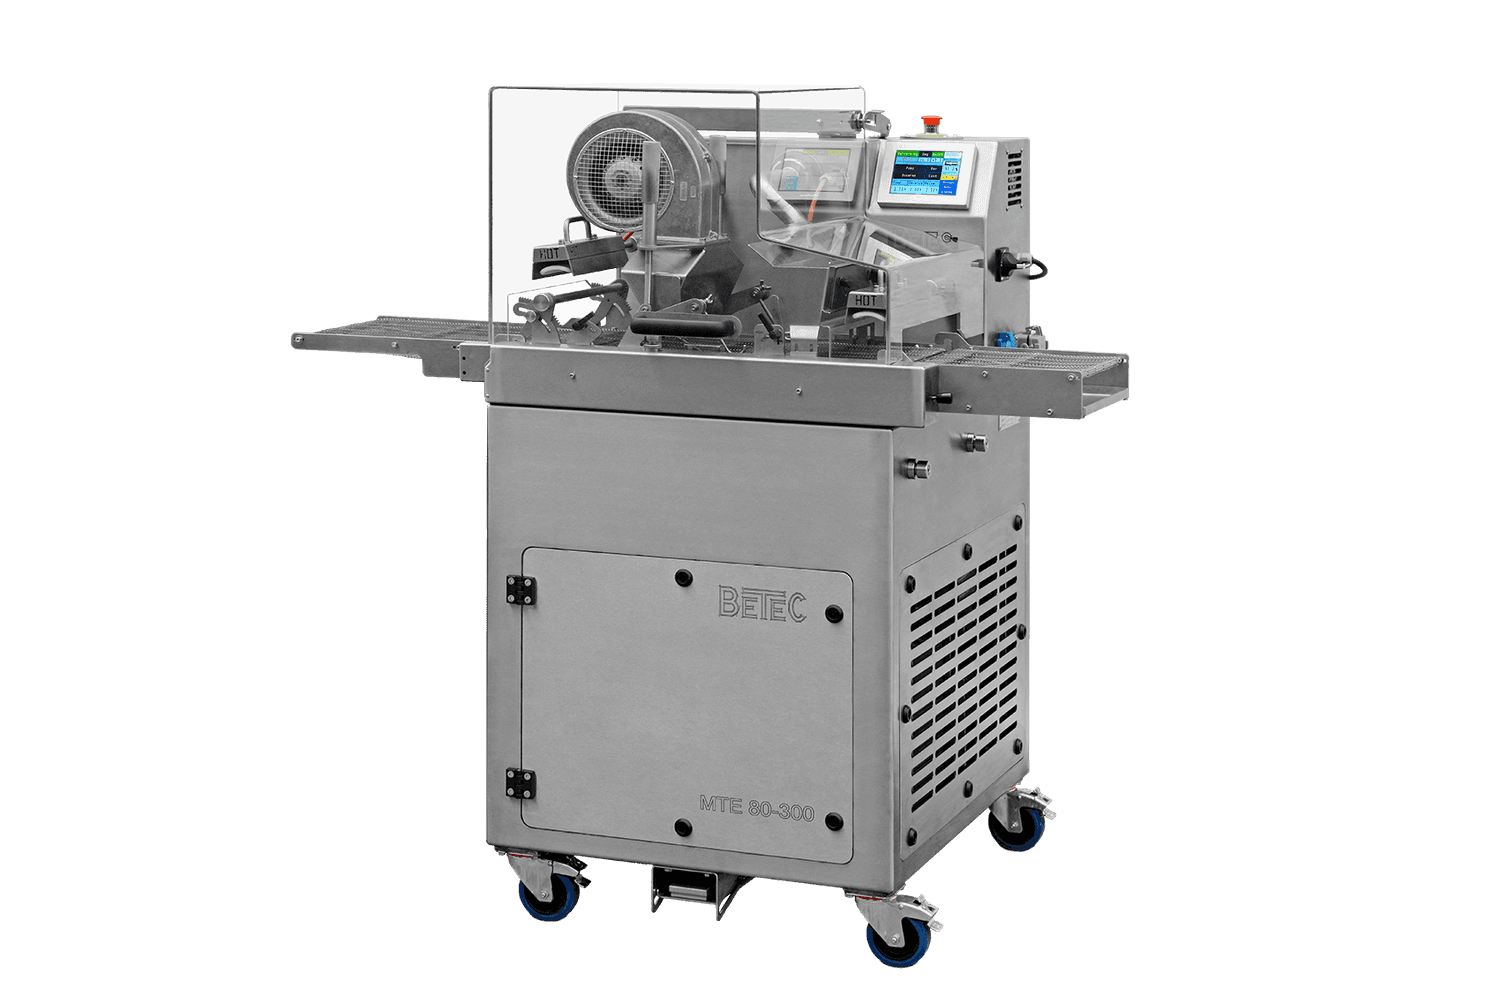
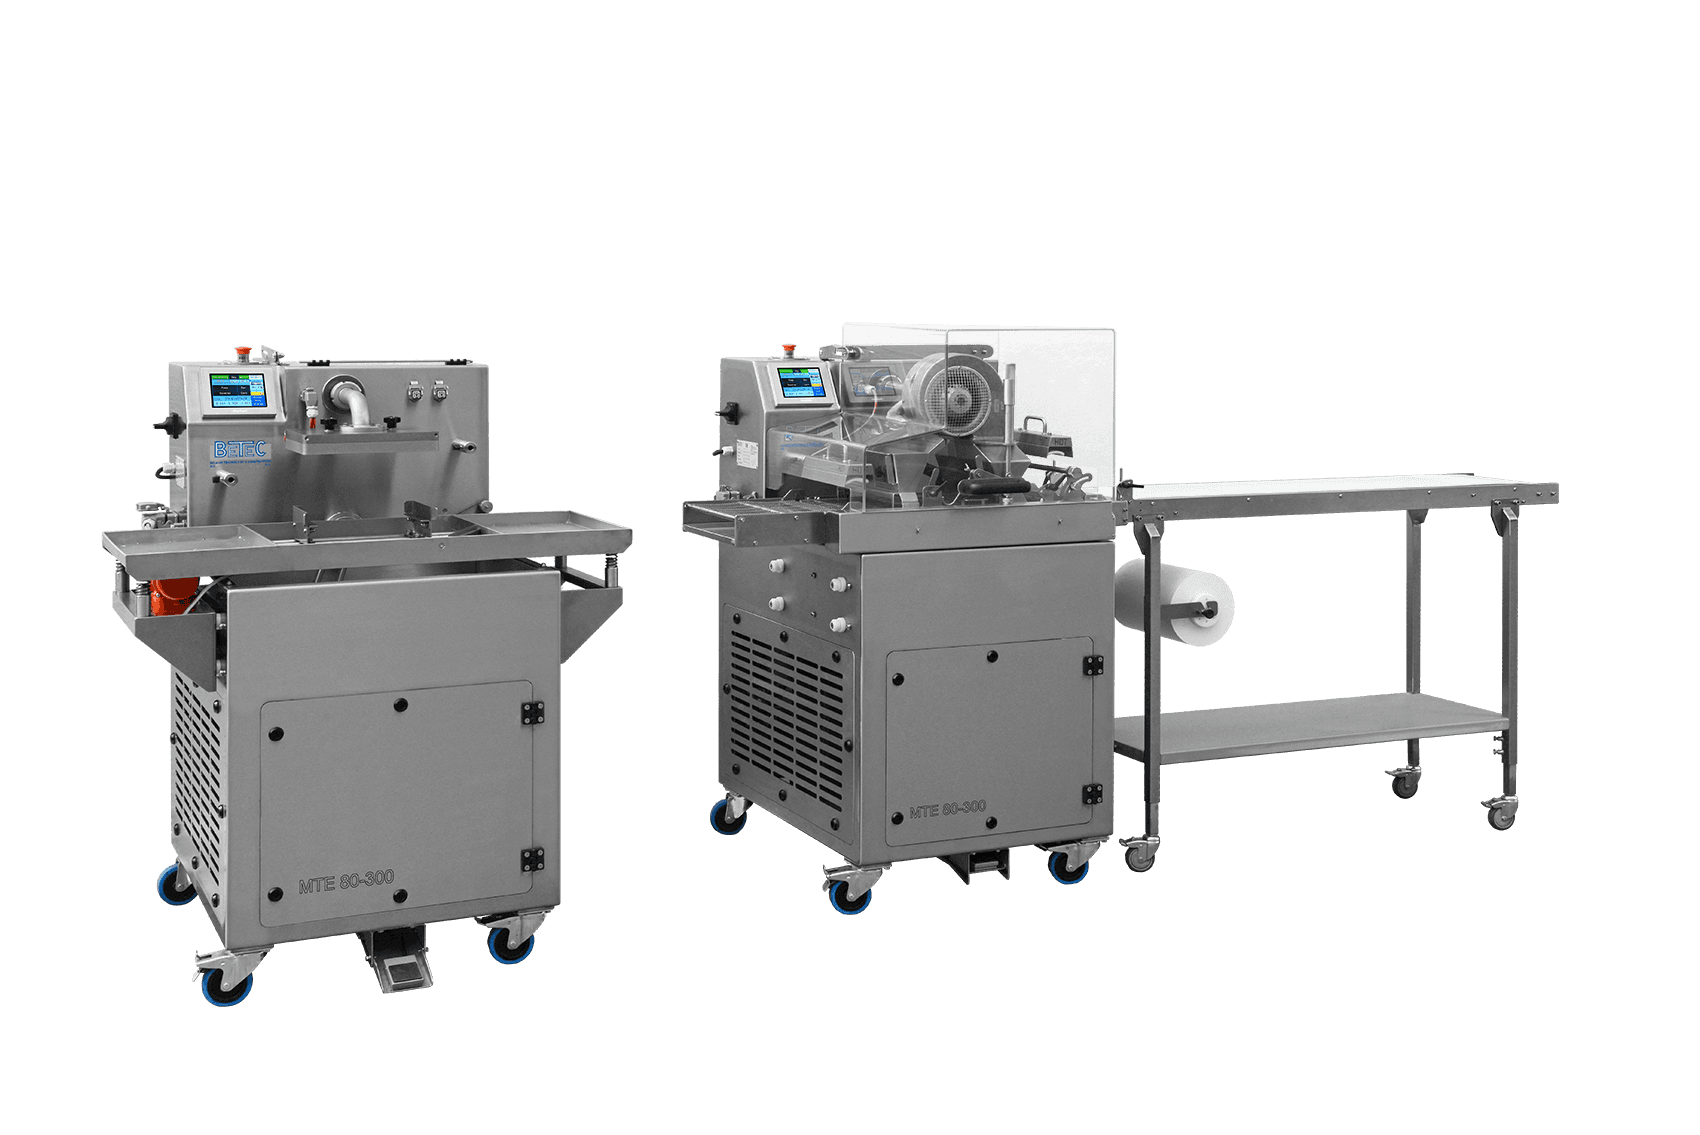
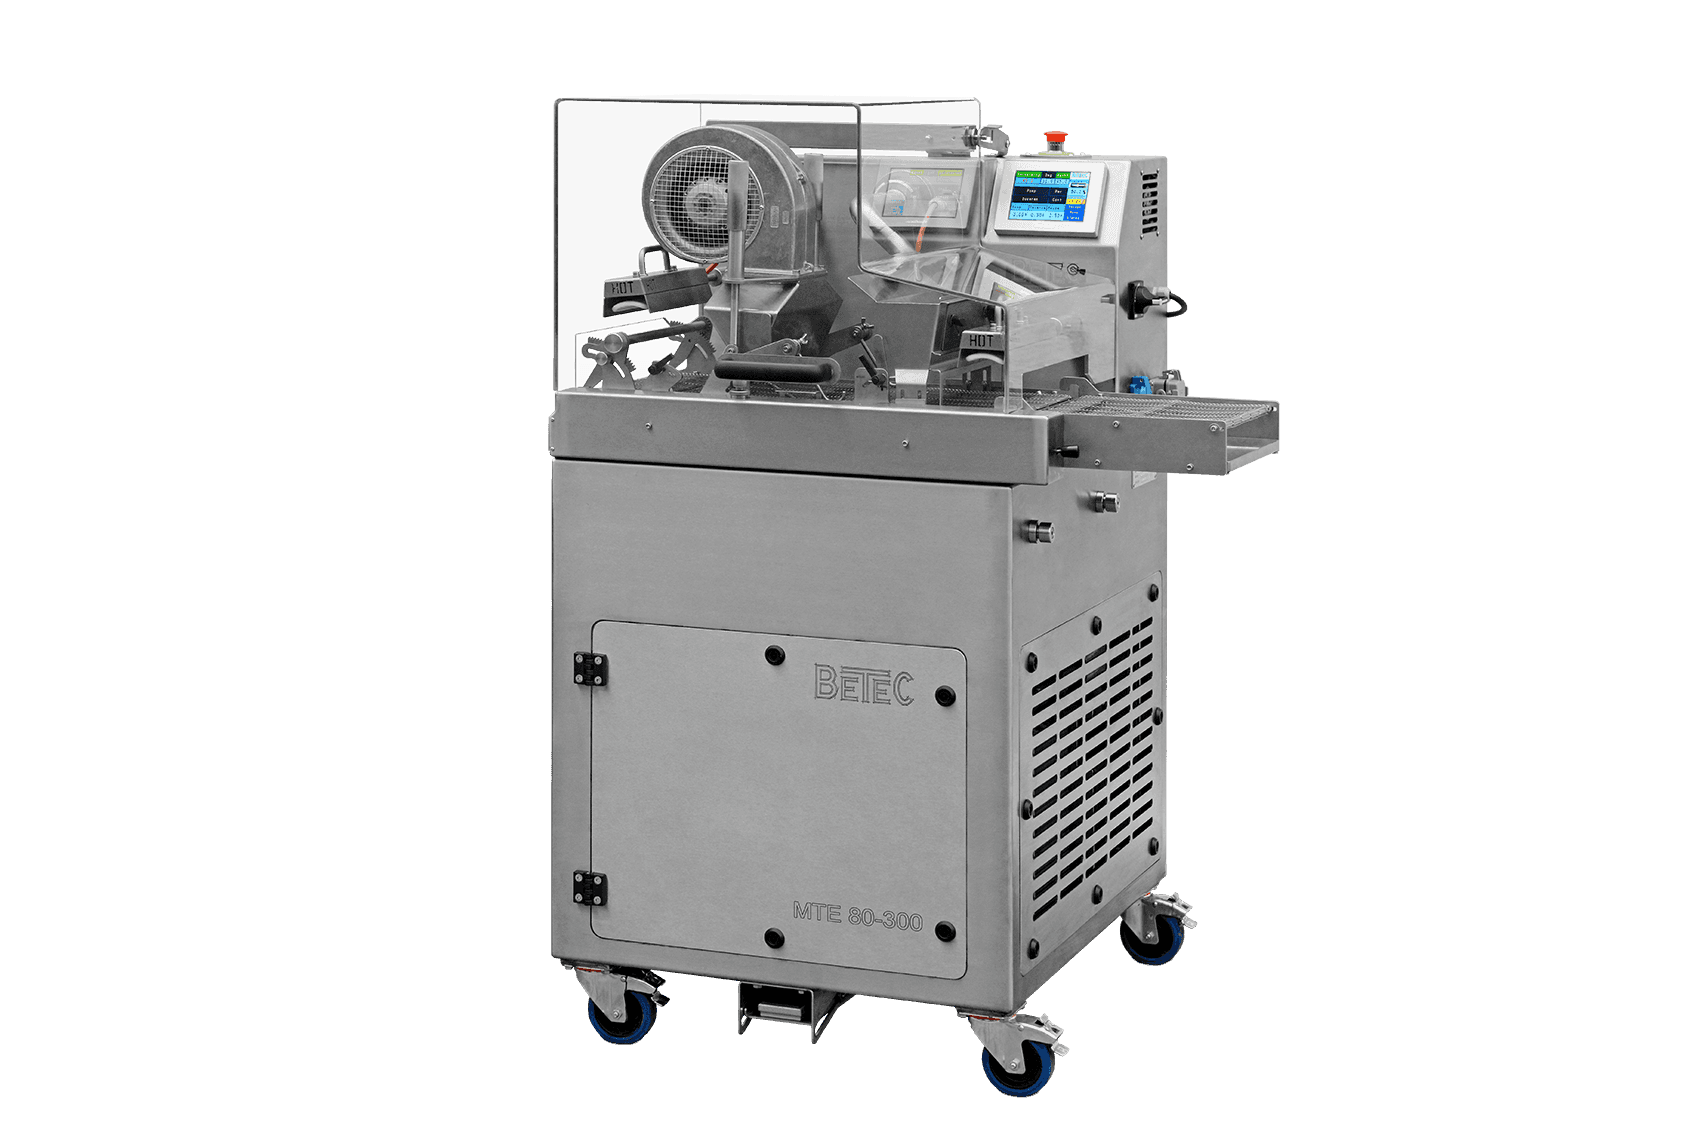
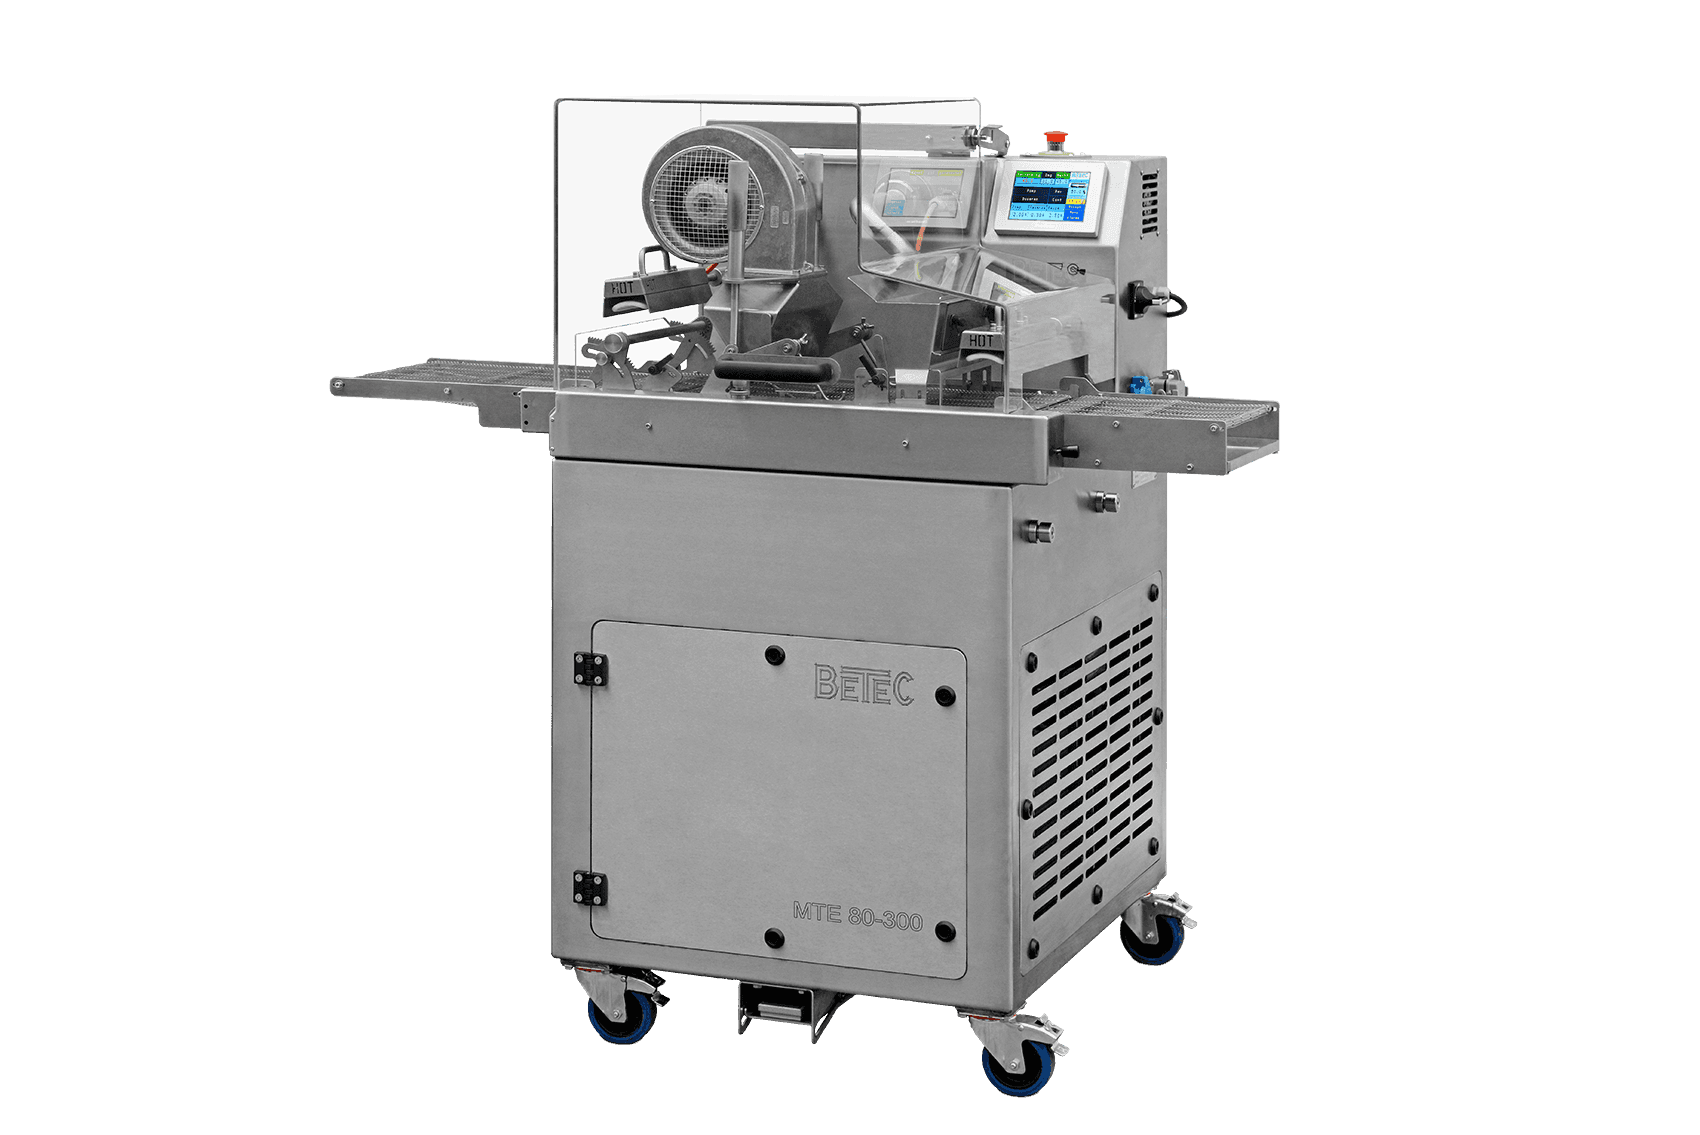
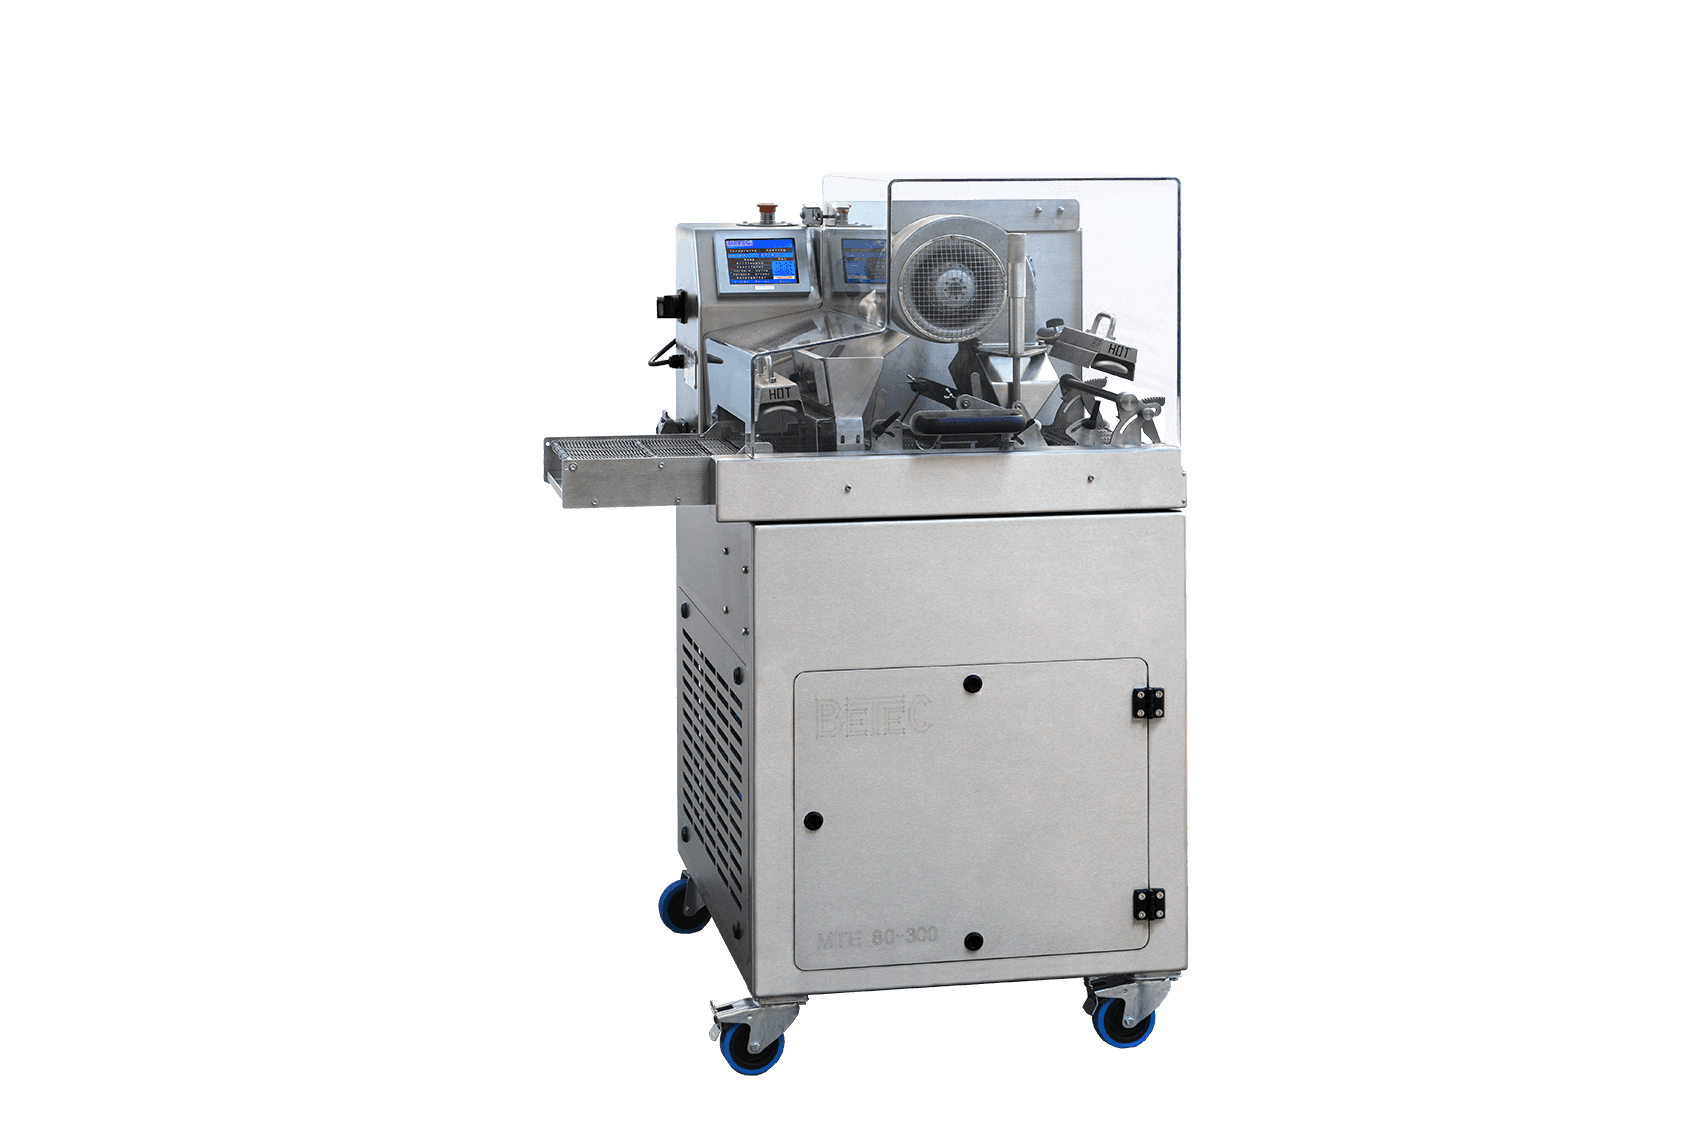
The model retains the versatility of the MT/MTE concept. The MT 80 combines continuous tempering with moulding and dosing on a heated vibrating table. The MTE 80 adds an enrobing belt for coating products with chocolate. In a 2-in-1 configuration, both components can be used alternately on the same core unit.
The larger chocolate supply and available working space provide more scope for applications requiring greater quantities of chocolate and larger working zones. The machine can be used both for individual operations and as part of a more extensive production configuration.
At higher chocolate consumption rates, an external melting or working tank can maintain the level in the chocolate tank in a controlled manner. The MT/MTE 80 can thus be incorporated into a configuration with a larger external chocolate supply and higher chocolate consumption, while retaining the series’ flexible working methods.
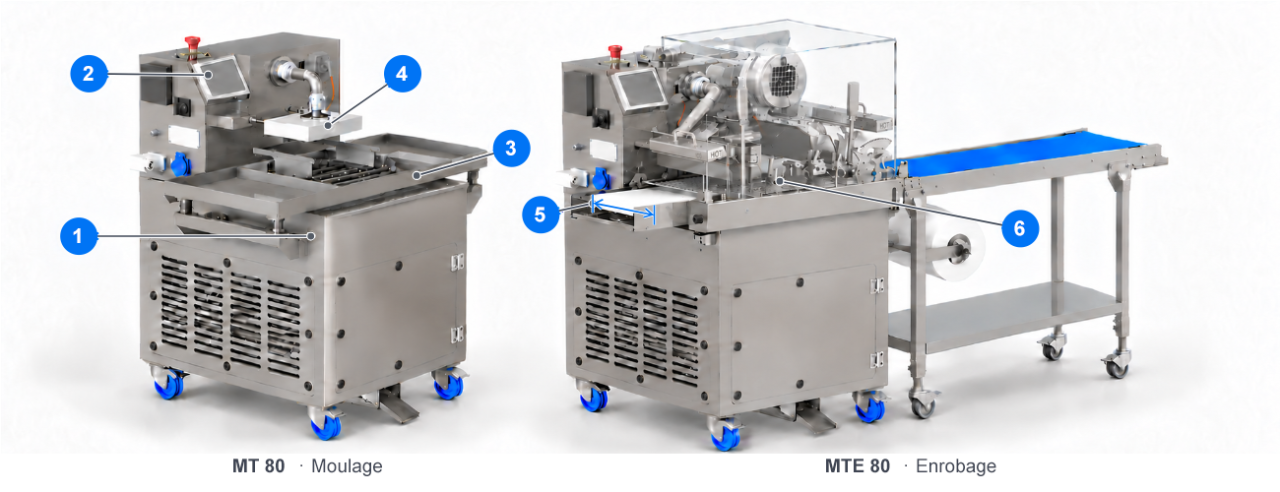
Key features of the MT/MTE 80
- Automatic tempering machine with an 80 kg chocolate capacity
- Central PLC control with a colour touchscreen
- MT version with a heated, adjustable vibrating table for moulding and/or dosing
- Controlled dosing with an optional dosing head and foot pedal
- Standard enrobing belt with a 400 mm working width, optionally available with a 300 mm or 240 mm working width
- Longest vibration zone in the MT/MTE series for targeted control of the chocolate coating and finish
- Robust core unit made from 3 mm thick AISI 304 stainless steel
- Electrically heated chocolate tank
- Archimedes screw for continuous chocolate circulation and tempering
- Suitable for chocolate with inclusions up to approx. 4–5 mm
- Largest version in the MT/MTE series, with more working space on the vibrating table and enrobing belt
- MTE version for continuous tempering and enrobing in a single process
- Enrobing belt with extensive adjustment options, developed using the same principles as our larger industrial enrobing lines
- 2-in-1 version for moulding, dosing and enrobing with the same core unit
- Easy changeover between vibrating table and enrobing belt, without special tools
- Option to prepare the MTE core unit for the later addition of an enrobing belt
- Can be combined with an external BETEC or Aura melting or working tank for controlled chocolate supply
- Easy operation, cleaning and maintenance
- 230 V – 50/60 Hz
Which MT/MTE suits your production?
The MT/MTE series is available in three sizes. Each size offers options for tempering, moulding, dosing and enrobing, including a flexible 2-in-1 configuration.
MT/MTE 15 — the most compact version
15 kg chocolate capacity. Standard enrobing belt width of 240 mm, also available in 180 mm. → View the MT/MTE 15
MT/MTE 35 — compact with a larger chocolate capacity
35 kg chocolate capacity. Standard enrobing belt width of 300 mm, also available in 240 mm. → View the MT/MTE 35
MT/MTE 80 — the largest version in the series
80 kg chocolate capacity and more available working space on the vibrating table and enrobing belt. Standard enrobing belt width of 400 mm, also available in 300 or 240 mm.
Continuous chocolate tempering from an 80 kg chocolate tank
A robust core unit made from 3 mm thick AISI 304 stainless steel forms the basis of the MT/MTE 80. The chocolate supply is kept at temperature in the electrically heated tank and fed from there through the tempering circuit.
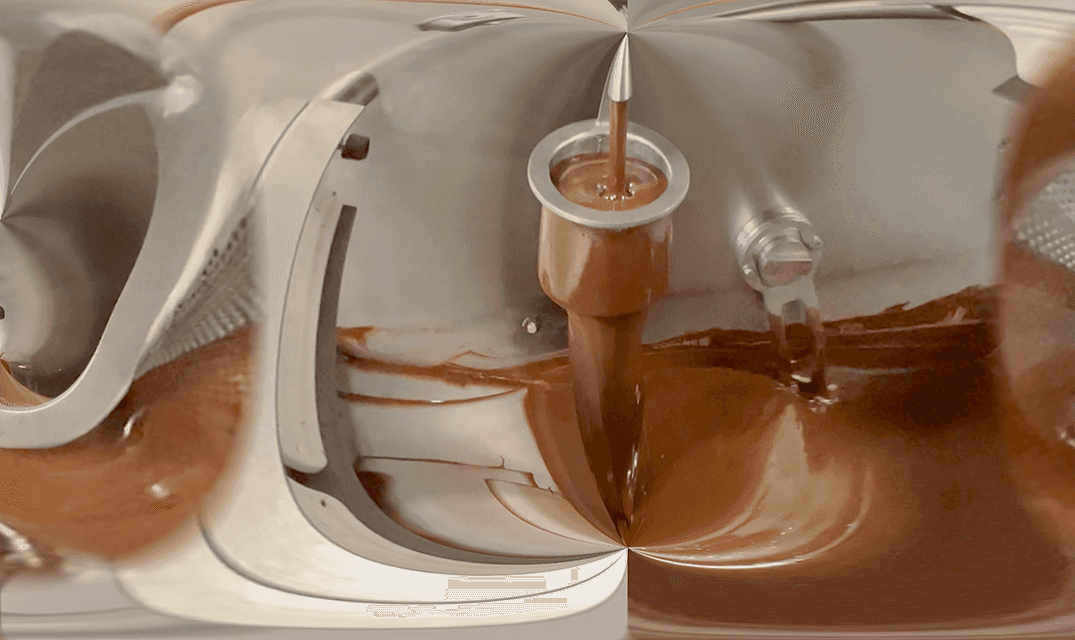
The chocolate reaches the Archimedes screw through the suction pipe, and the screw carries it upwards through the cylinder. Around the screw, this cylinder acts as the tempering column. Transport and tempering therefore take place together in a single continuous process.
As it passes through the tempering column, the chocolate is cooled and tempered under controlled conditions. At the top, it leaves the machine through the outlet, to which the required outlet pipe or an optional dosing head can be fitted. Unused chocolate returns to the tank and is recirculated.
The operator monitors the process via the central PLC control with colour touchscreen. Temperatures and machine functions can be monitored, set and saved here, keeping operation centralised on the core unit.
Tempering and processing chocolate with inclusions
The MT/MTE 80 can also process chocolate with small inclusions up to approximately 4–5 mm. The Archimedes screw transports the chocolate through the machine, eliminating the need for a conventional chocolate pump.
Nut pieces, crunchy ingredients and other small inclusions remain in the mixture while the chocolate circulates and is tempered.
This makes it possible to produce chocolate bars and other moulded products with inclusions directly from the machine, for example.
External chocolate supply at higher consumption rates
The MT/MTE 80 can be connected to an external BETEC or Aura melting or working tank. Particularly at higher chocolate consumption rates, a working tank with a chocolate pump can maintain the level in the chocolate tank in a controlled manner.
The external tank supplies chocolate at a low, constant flow rate according to consumption. This avoids having to add large quantities of chocolate all at once. This controlled supply helps limit unnecessary temperature fluctuations caused by large additions and their impact on the tempering process.
The MT/MTE 80 can thus be integrated into more extensive production configurations with a larger external chocolate supply and higher chocolate consumption.
MT 80 – more working space for chocolate moulding and dosing
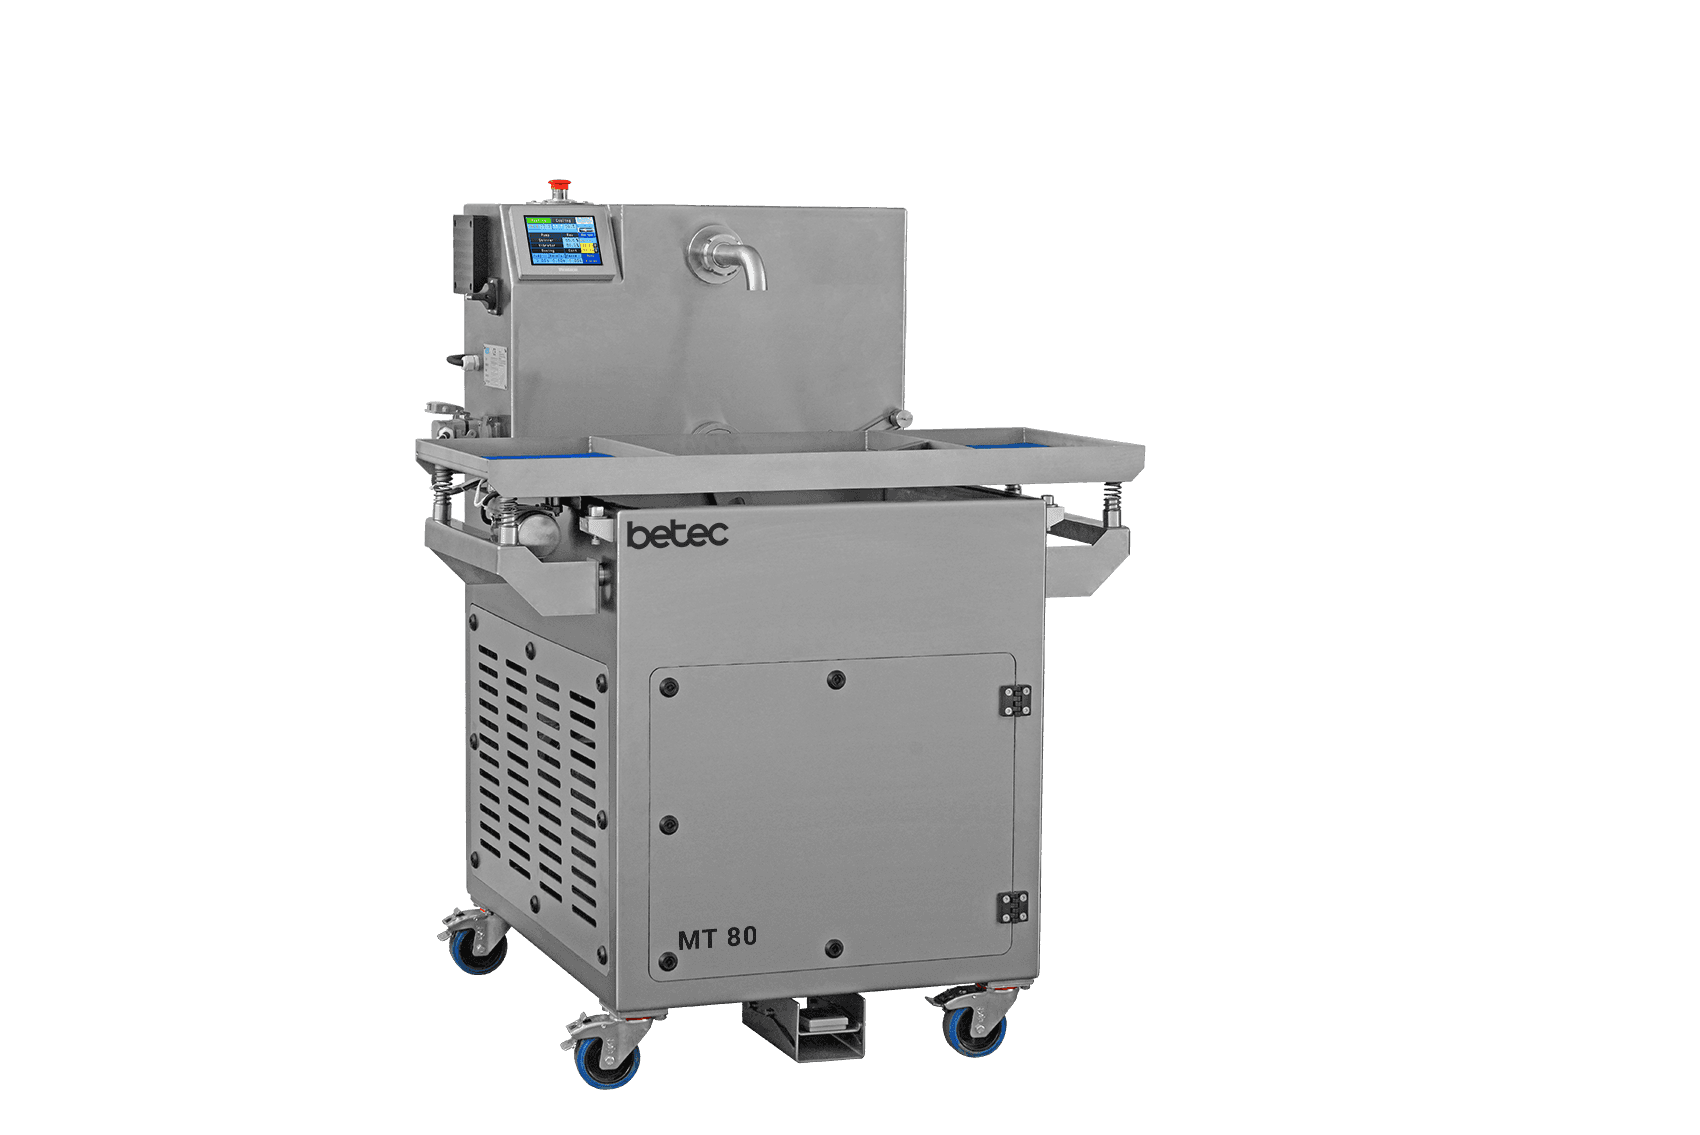
The MT 80’s heated vibrating table provides more available working space within the MT/MTE series. Moulds are filled with tempered chocolate directly from the machine and can be vibrated during or immediately after filling.
The vibrating table is electrically heated to prevent chocolate on the work surface from setting too quickly. Both the temperature and the vibration motor’s vibration frequency are continuously adjustable via the core unit’s touchscreen.
The scraper blade position can be adapted to the application and the operator’s preference, for example for left- or right-handed use. Optional positioning supports allow a mould to be placed quickly and accurately in the same position each time. When using dosing heads, this helps align the mould correctly beneath the nozzles.
To connect the vibrating table, it is placed on the core unit and connected with a single plug. The heating and vibration functions are then controlled via the touchscreen. The table can also be easily removed again.
These supports allow the mould to remain on the vibrating table during dosing. The chocolate is then distributed immediately across the mould while air bubbles escape more easily. Vibration thus supports faster, more even filling and helps reduce trapped air in the finished product.
A suitable optional dosing head on the chocolate outlet enables controlled dosing. The operator sets the dosing time on the touchscreen and starts dosing with the foot pedal. Both hands remain free to position and move the mould.
For applications requiring advanced and highly accurate dosing capabilities, the MT/MTE series also includes the dedicated MT 80 GPE/GPI versions.
View the full MT 80 GPE/GPI description for more information on these dosing capabilities.
MTE 80 – continuous enrobing with the longest vibration zone in the series
For enrobing, the MTE 80 core unit is combined with a BETEC enrobing belt. The name MT is derived from Mini Temper (Mini Tempering Machine). The additional E stands for Enrobing.
Above the chocolate tank, the enrobing belt receives tempered chocolate directly from the core unit. Chocolate circulation and tempering continue during enrobing, so that tempering and enrobing take place in a single continuous process.
The MTE 80 has the longest vibration zone in the MT/MTE series. This provides more space and time to influence the chocolate coating after application, before the product leaves the machine. Vibration can therefore be used more precisely to achieve the required coating thickness and finish.
Depending on the chosen settings, products can be fully enrobed or, for example, receive a chocolate coating only on the underside (bottom coating).
An optional adapted chocolate curtain trough also allows the chocolate flow to be divided into separate zones across the belt width. Products can therefore be partially coated according to a predetermined pattern, for example when only part of a biscuit or other product needs to be covered with chocolate.
MTE 80 – chocolate enrobing with control over coating thickness and finish
The MTE 80 allows products to be continuously enrobed with tempered chocolate. The various stages of the enrobing process are individually adjustable.
The enrobing belts in the MT/MTE series are built using the same basic principles as our larger industrial enrobing lines. The MTE 80 therefore also offers extensive adjustment options for targeted control of coating thickness, chocolate distribution and finish, among other aspects.
By combining the various settings and adjustment options, the chocolatier can refine the enrobing process step by step. Parameters such as speed, airflow, vibration and other controls can be adjusted individually and coordinated to work towards the desired result.
The desired product result comes first: the enrobing belt is adjusted to suit it, rather than the other way round.
Electronic settings are adjusted directly and continuously via the core unit’s touchscreen. Mechanical adjustments are made on the enrobing belt itself.
Adjustable belt speed
The belt speed is continuously adjustable via the core unit’s touchscreen. This allows the operator to match the conveying speed to the product and the required production capacity.
Adjustable chocolate curtain
The chocolate curtain applies tempered chocolate to the products from above. The quantity of chocolate is adjusted mechanically at the curtain trough to match the chocolate flow to the product. By raising or lowering the curtain trough, the distance between the trough and the top of the product can be adapted to the product height.
Adjustable bottom-coating bath
The bottom-coating bath applies chocolate to the underside of the product. Two mechanically adjustable flaps on the wire mesh belt control the quantity of chocolate used for this bottom coating.
Adjustable air-blowing system
After the product passes through the chocolate curtain, the air-blowing system removes excess chocolate. The air speed is continuously adjustable via the touchscreen. The height and angle are adjusted mechanically on the wire mesh belt.
By coordinating these settings, the operator can adapt the air blowing to the shape of the product and the required thickness and finish of the chocolate coating.
Adjustable vibration
The controlled vibration of the wire mesh belt removes excess chocolate and helps the remaining chocolate flow out evenly. Vibration thus contributes to a level, mirror-smooth top surface on the enrobed product.
The vibration intensity is set mechanically on the enrobing belt and matched to the product and the desired chocolate coating.
The MTE 80 has the longest vibration zone in the MT/MTE series. The longer distance over which products are subjected to controlled vibration provides additional scope to influence coating thickness and finish through the vibration intensity.
Compensation roller
The compensation roller spreads chocolate evenly across the underside of the product and helps prevent an excessively thick chocolate base. The roller can also smooth over a small gap in the chocolate base. In this way, it compensates for irregularities in the bottom coating.
The compensation roller is mounted on a fixed shaft and is not adjustable. A mechanism in front of the roller allows the wire mesh belt to be raised, so that the products pass above the roller without touching it. Raising or lowering the wire mesh belt allows the compensation function to be disengaged or engaged.
Heated detailer
At the transfer to a take-off conveyor or cooling tunnel, the heated detailer removes excess chocolate from the trailing edge of the product’s underside. This reduces the formation of unwanted chocolate tails and produces a neater finish. At the same time, the detailer helps keep the downstream take-off conveyor or cooling tunnel conveyor belt cleaner, as less excess chocolate is carried over.
The operator sets the detailer’s temperature and direction of rotation via the touchscreen. Its height is adjusted mechanically on the wire mesh belt to suit the product.
Heated zone beneath the acrylic cover
Beneath the acrylic cover, the MTE 80 has two independently adjustable infrared heaters: one at the infeed and one at the outfeed. Both heaters are continuously adjustable via the touchscreen, allowing the temperature at each end of the enrobing belt to be matched independently to the product and process.
The infrared heater at the infeed can be used, for example, to warm heavily chilled products slightly and in a controlled manner before enrobing. This reduces the temperature difference between the product and the tempered chocolate and prevents the chocolate from starting to set too quickly on contact. It gives the air-blowing and vibration systems more opportunity to refine the chocolate coating further.
The infrared heater at the outfeed helps keep the transfer area to a take-off conveyor, cooling tunnel or truffle attachment, for example, at temperature. This helps prevent the chocolate from cooling too quickly at this transfer point and starting to set on the nose of the enrobing belt.
Both heating zones can be adjusted independently to suit the application. Heating must always remain controlled: excessive heating can disrupt the crystal structure formed during tempering, affecting the final setting and finish of the chocolate.
Independently controlled and easily removable infeed belt
The infeed belt can be switched on and off independently. This allows the operator to control product infeed without switching the rest of the enrobing belt on or off at the same time.
The infeed belt can be easily removed for cleaning. This improves access to the infeed area and makes the infeed belt easier to clean.
The MTE 80’s standard enrobing belt has a working width of 400 mm. Optional working widths of 300 mm or 240 mm are available to suit the application and the required configuration.
MT/MTE 80 2-in-1 – moulding and enrobing on one core unit
The MT/MTE 80 can also be supplied in a 2-in-1 configuration, combining moulding and enrobing without the need for two separate tempering machines.
The MT/MTE 80 2-in-1 uses one core unit, on which the vibrating table and enrobing belt are used alternately. Four spring-loaded legs support the vibrating table on removable supports. When production changes from moulding to enrobing, the vibrating table is removed and the enrobing belt takes its place above the chocolate tank.
Changing between the vibrating table and enrobing belt has been kept deliberately simple and can be carried out by the operator, without special tools or technical knowledge. The vibrating table is removed and the enrobing belt is moved into position. With the larger 400 mm enrobing belt, an extra pair of hands can of course be useful – for convenience, rather than technical assistance.
The same core unit can thus be used alternately for moulding and dosing or for continuous enrobing, depending on what is being produced at the time.
Mould today, enrobe later
A complete 2-in-1 configuration can also be built up in stages. In this case, the machine is supplied with a prepared MTE core unit from the time of purchase, but initially fitted only with the vibrating table.
In this initial phase, the configuration operates like an MT 80 for tempering, moulding and, if required, dosing. A suitable BETEC enrobing belt can be added later when enrobing becomes part of the production process.
For this expansion, the choice of core unit at the time of purchase is decisive. A standard MT 80 core unit cannot subsequently be converted into an MTE version. Anyone wishing to add an enrobing belt later should therefore choose the prepared MTE core unit from the outset.
Options and accessories
Options and accessories allow us to adapt the MT/MTE 80 further to your products and the way you want to work.
Depending on the chosen version, various dosing heads, dosing nozzles and accessories for moulding and enrobing are available.
The following additions can also be provided for specific tasks:
- Bucket support with adapted outlet – allows tempered chocolate to be drawn off directly from the machine into a bucket easily and in a controlled manner.
- Chocolate sieve – fitted to the outlet pipe, it filters crumbs and other impurities from the circulating chocolate. This is useful when enrobing biscuits or other products that may introduce small particles into the chocolate.
- Dipping tray – provides a continuous supply of fresh tempered chocolate for manually dipping products such as orange slices.
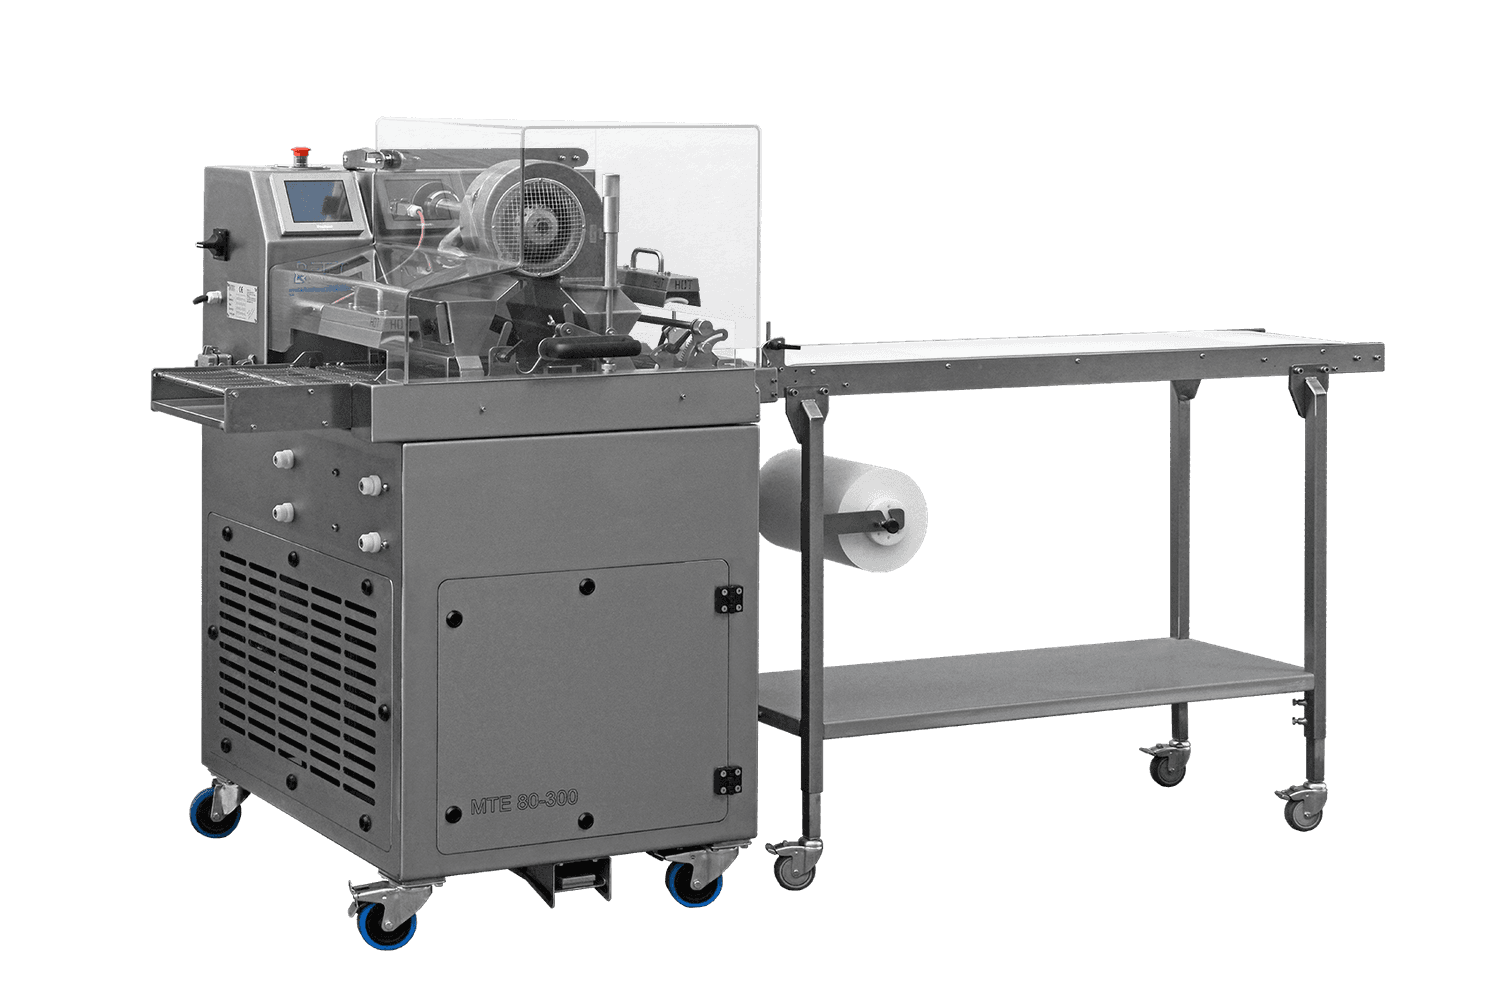
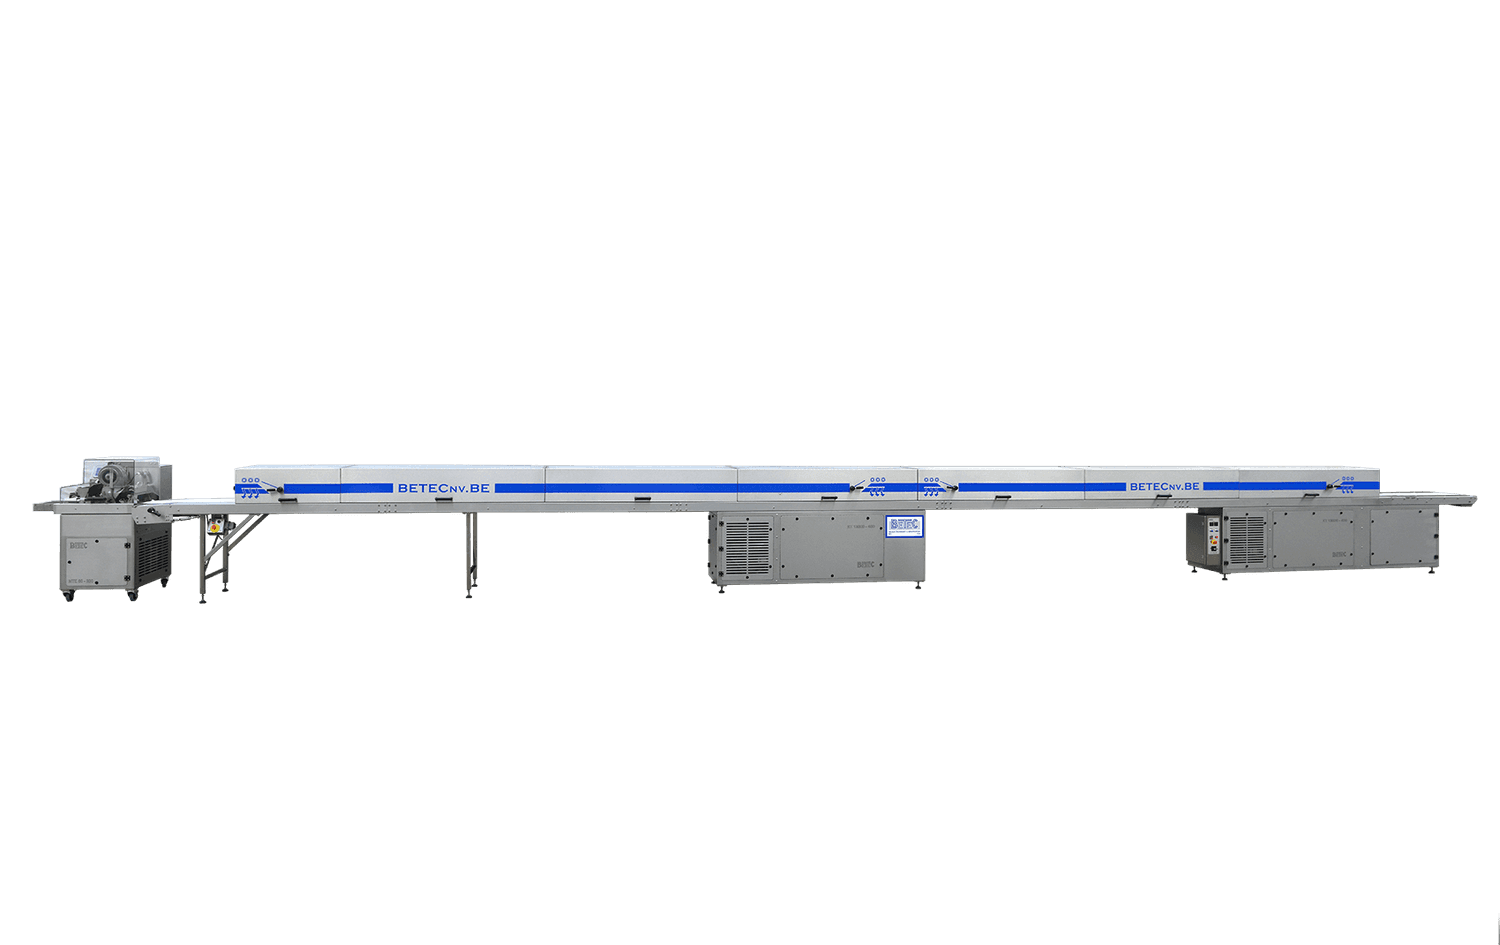
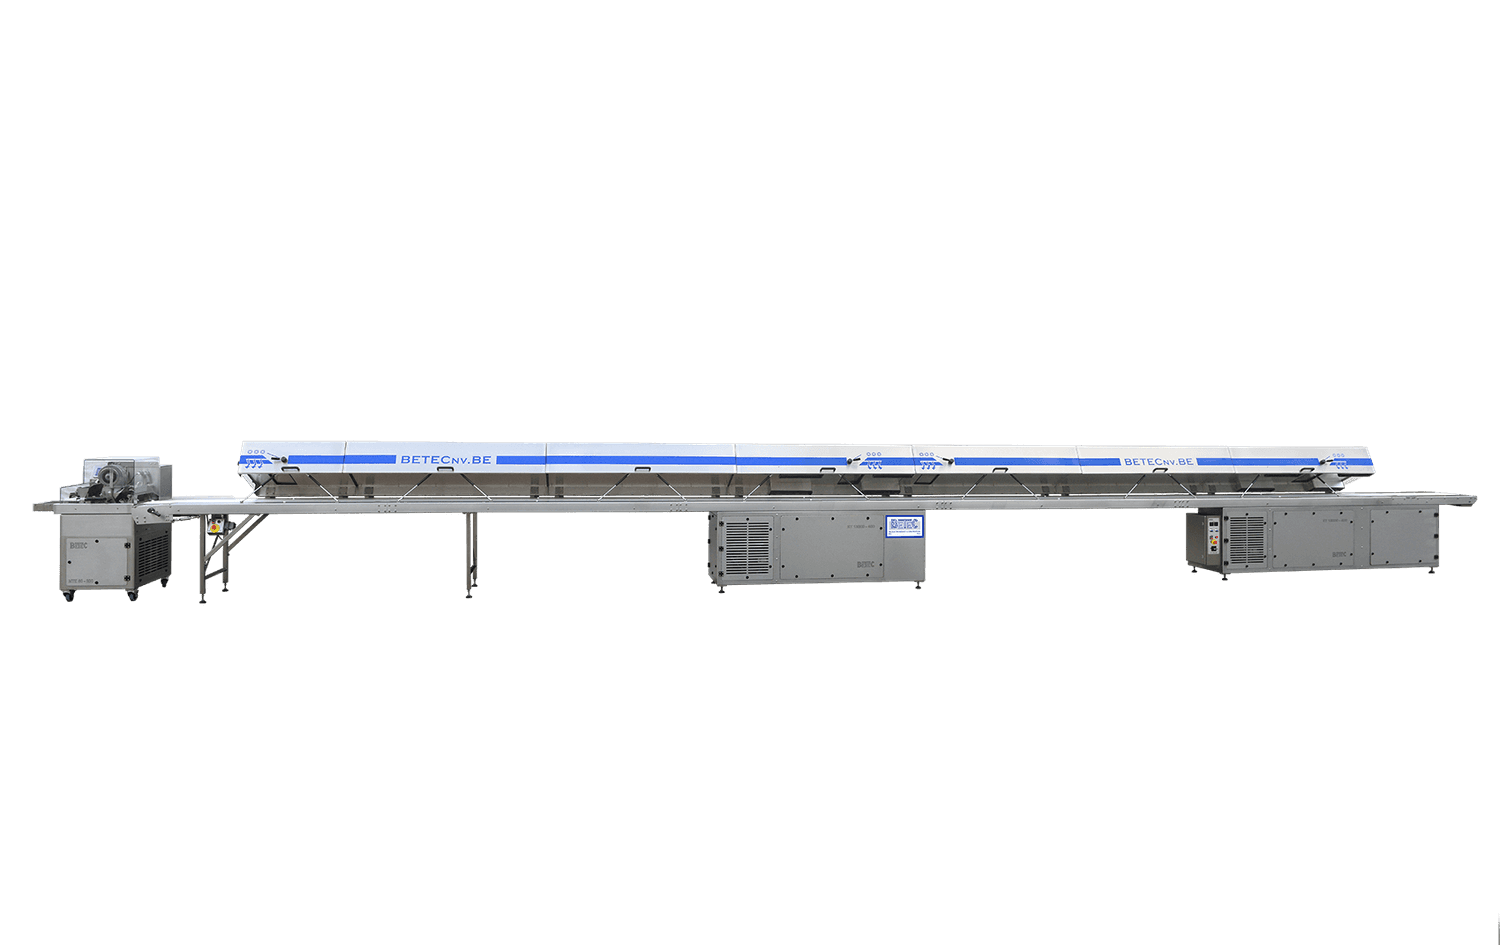
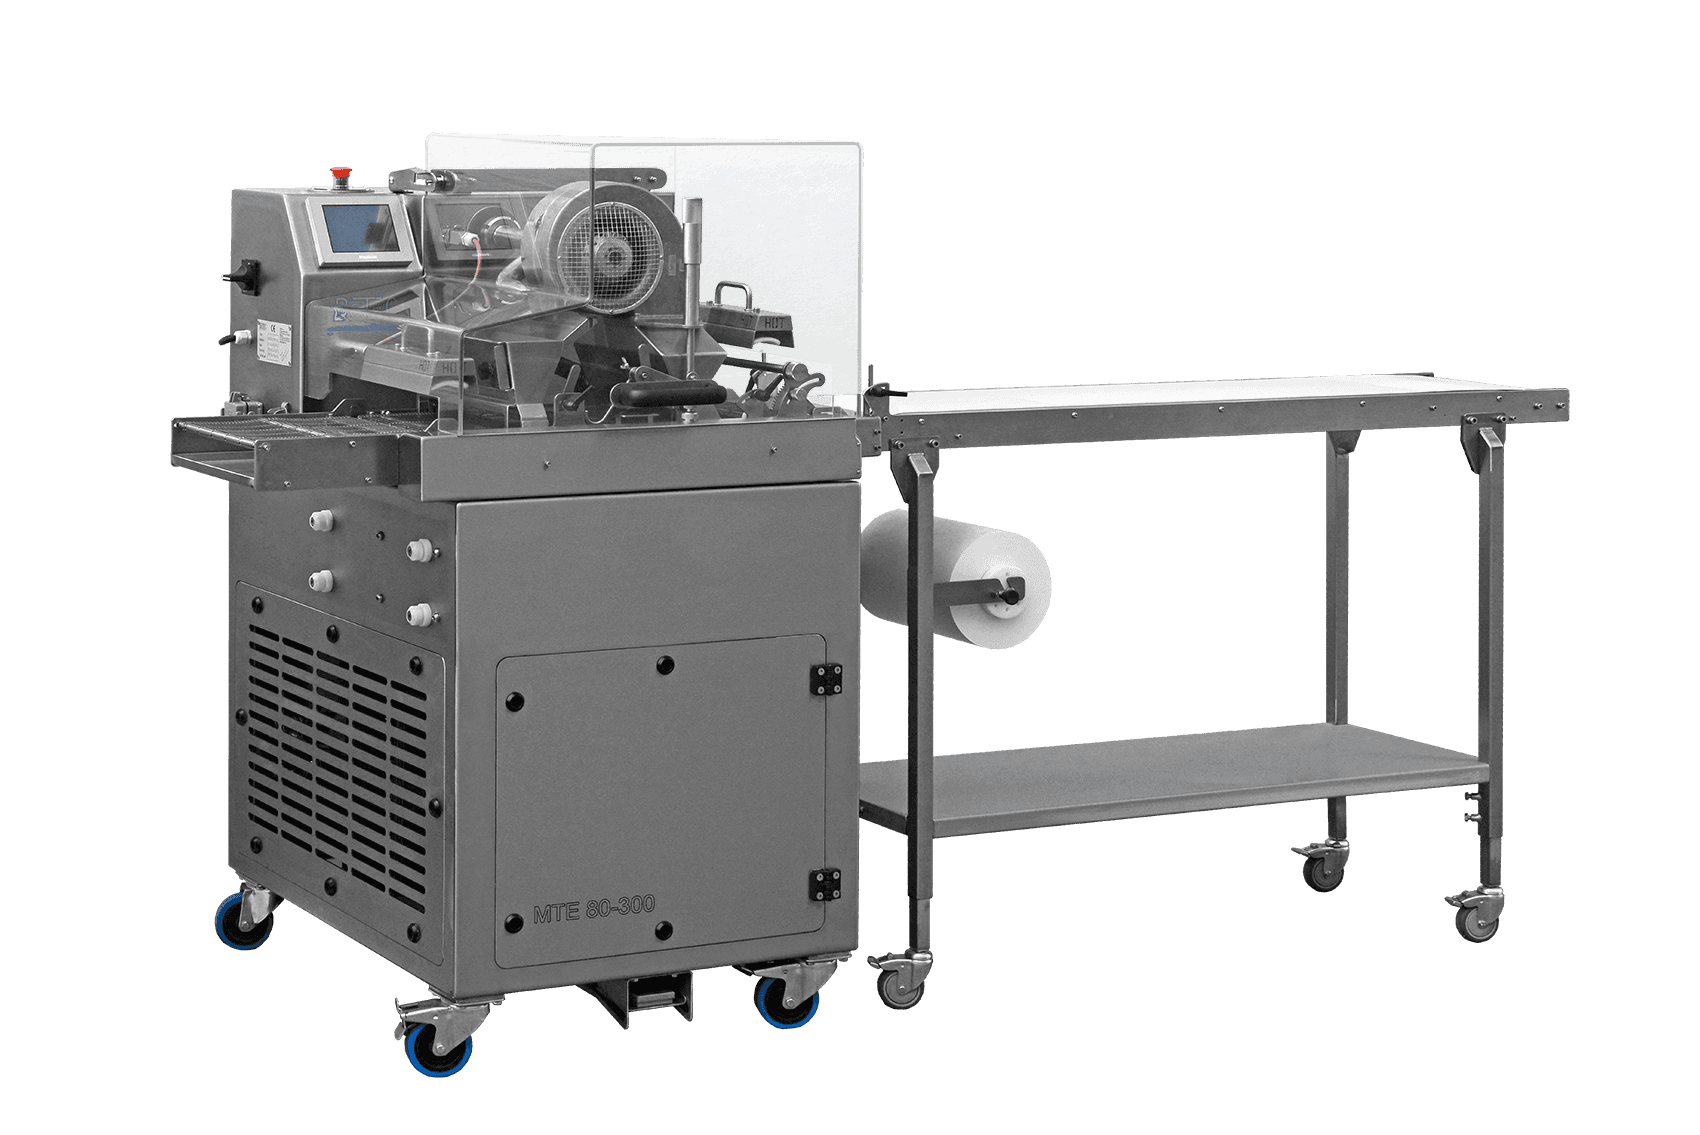
- TOC-…-1500 take-off conveyor with paper roll – a practical solution after the enrobing belt when no cooling tunnel is used. Freshly enrobed products are carried onwards on glassine paper, allowing the enrobing belt to continue producing. The aluminium support plate beneath the paper allows the products to be transferred easily to a trolley or drying rack to finish setting. The take-off conveyor has a standard length of 1.5 metres and an adjustable nose for precise transfer from the enrobing belt. For smaller production runs, this can be a compact and economical solution where the investment or space required for a cooling tunnel is not desirable.
- GT-MT ganache table – mounted above the enrobing belt’s infeed belt, it creates a practical working area for placing and feeding ganache and other products. This removes the need for a separate table beside the machine and allows the operator to work more ergonomically in a smaller space.
- Truffle attachment for the enrobing belt – an addition for chocolate truffle production that provides a controlled transfer between the enrobing belt and a cocoa powder or finishing table. The nose is adjustable and the truffle attachment is easy to fit to and remove from the enrobing belt.
- RT 1000 rotary, buffer and finishing table – can be positioned after the truffle attachment, among other uses, for further finishing of truffles with cocoa powder or chocolate flakes, for example. The rotary table can also be used as a buffer or packing table and is adapted to the required application.
- MCP-3X manifold for thick chocolate – distributes thicker chocolate evenly across the enrobing belt’s buffer bath. Three individually adjustable valves allow the chocolate flow to be controlled and the buffer bath to be supplied evenly across its full width. The manifold can be fully dismantled for easy cleaning.
- Dosing heads for tempered chocolate – for accurate mould filling, the MT/MTE can be equipped with various dosing heads. The CMDH (Custom Made Dosing Head) is made to suit the polycarbonate mould used and distributes the chocolate according to its fixed pattern. For hollow figures and moulds with varying filling positions, the EAD (Easy Adjustable Dosing Head) offers flexible, easily adjustable tubes that can quickly be aligned with the required filling positions. Both dosing heads are electrically heated as standard and can be supplied with a snaplock or threaded connection.
Various additions are also possible for other specific moulding, dosing and enrobing applications.
Please contact us. Together, we can determine which version and options best suit your products and production process.
Photos






Videos